Substrate Entry Conditions
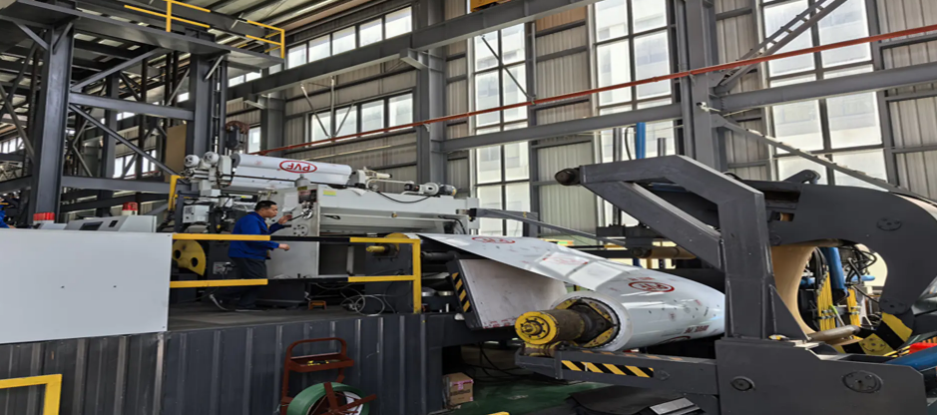
An Aluminum Coil Coating Line receives coils with various tempers—from soft O-temper to hard H19. The temper influences how the strip behaves under tension and heat. Soft alloys elongate more during oven heating, requiring a higher dancer roller position to absorb slack. Hard alloys resist stretching but may transmit vibrations back to the coater. Thus, the line speed is set not only by oven capacity but also by alloy characteristics. At the entry, a leveler flattens the coil head, removing coil set. This leveler consists of six offset rolls that bend the strip alternately up and down, reducing internal stress. After leveling, a notcher cuts the leading edge for a clean splice. The splice is welded with a tungsten-inert-gas torch, then the weld bead is ground flush to avoid marking the coater rolls. This entire entry sequence takes less than two minutes, thanks to a dual-mandrel unwinder that prepares the next coil while the current one runs.
In the coating section, the choice of resin dictates the oven temperature ramp. For high-gloss architectural panels, a linear ramp from 20°C to 240°C over 40 seconds works well. For matte finishes, a slower ramp with a longer hold at 180°C encourages controlled flow and leveling. The oven controllers use a cascade loop—one loop regulates the burner firing rate based on zone temperature, and a second loop trims based on strip temperature measured by a pyrometer. If the pyrometer indicates the strip is too hot, the line speed increases slightly, reducing dwell time. Conversely, a cold strip triggers a speed reduction. This dynamic adjustment maintains a constant peak metal temperature (PMT), which is critical for cure degree. Under-cured films show poor solvent resistance; over-cured films become brittle. A simple rub test with methyl ethyl ketone checks cure—fifty double-rubs without breaking the film indicate sufficient crosslinking.
After cooling, a protective peelable film may be laminated onto the coated surface for shipping. This film guards against handling scratches during slitting and transportation. The laminator applies the film with a rubber nip roll; tension between the film and the strip must match to avoid wrinkles. Finally, the coil edges are trimmed by rotary shears, and the scrap edge is chopped into small pieces for recycling. The finished coil's inner diameter, outer diameter, and weight are recorded. For customers who will later stamp or emboss the coated sheet, the line provides a flexibility test result—bending the sample over a 3T mandrel without cracking. An Aluminum Coil Coating Line must accommodate diverse end uses, from curtain walls to beverage can ends, each requiring distinct coating hardness and elongation properties. Therefore, the line staff maintains a library of cure schedules, indexed by resin type and gauge. Changing from one schedule to another involves loading a pre-set recipe from the distributed control system, which adjusts all zone temperatures, fan speeds, and line speed simultaneously.
 English
 Arabic
 French
 Spanish
 Portuguese
 Deutsch
 Turkish
 Dutch
 Italiano
 Russian
 Romaian
 Portuguese (Brazil)
 Greek
